
What Quality Controls Should a Bearing Retainer Factory Apply Before Shipment?
A bearing retainer can appear to be a simple stamped, machined, molded, or formed component, yet a defect in the cage may lead to rolling-element instability, excess friction, lubricant starvation, abnormal noise, overheating, or early bearing seizure. Before shipment, a bearing retainer factory should therefore release parts only after confirming that the delivered lot matches the approved drawing, material specification, process route, inspection plan, and packaging requirements.
The critical point is that dimensional acceptance alone is not enough. A cage may pass a limited diameter check while still carrying burrs, cracked bridges, distorted pockets, incomplete heat treatment, contamination, or mixed material lots. These defects become especially serious in high-speed, high-load, high-temperature, vibration-sensitive, or safety-critical bearing applications. A reliable pre-shipment control system must connect each finished shipment to traceable evidence from incoming material through final packing.
Release should begin with controlled traceability, not final inspection alone
Every shipment should be traceable to a defined manufacturing lot. The lot definition needs to be practical and unambiguous: it may be based on one material heat, one molding batch, one heat-treatment batch, one production shift, or another documented grouping that allows effective containment if a nonconformity is found. Mixing parts from different lots without preserving identification makes later failure analysis and recall action unnecessarily difficult.
At minimum, release documentation should link the finished retainers to the following records:
- approved part number, drawing revision, and customer specification revision;
- purchase and receiving records for strip, bar, tube, polymer resin, or other raw material;
- material certificate or certificate of conformity where contractually required;
- manufacturing batch, machine or tooling identification, and production date;
- heat-treatment, coating, deburring, washing, or stabilization records where applicable;
- inspection results, nonconformance dispositions, rework records, and final release authorization;
- packaging lot and shipment identification.
Material certificates must be reviewed against the actual retainer specification rather than filed as an administrative formality. Chemical composition, mechanical properties, temper, condition, resin grade, reinforcement content, or heat number may all matter depending on cage design. For steel cages, the specified grade and delivery condition affect formability, strength, coating response, and subsequent heat treatment. For brass cages, alloy composition can influence machinability and resistance to certain lubricants or environments. For polymer cages, resin identity, glass-fiber content, moisture condition, and approved regrind limits can materially affect dimensions and mechanical behavior.
A certificate from a material supplier does not automatically prove that the factory used the correct material in production. Positive material identification, controlled material labeling, segregated storage, barcode tracking, and documented line clearance are valuable where the risk of material mix-up is significant. Material substitution should never be accepted merely because two grades appear commercially similar.
Geometry control must reflect how the cage functions inside the bearing
A retainer does not operate as an isolated part. It positions and separates rolling elements while maintaining clearance from bearing rings, seals, shields, and adjacent machine components. The inspection plan should therefore focus on functional geometry, not only on dimensions that are easy to measure.
Key characteristics commonly include bore diameter, outside diameter, cage width, pocket pitch, pocket diameter or contour, bridge thickness, rivet-hole position, tab geometry, flange height, concentricity, roundness, and total runout. Which dimensions are critical depends on the cage type: pressed steel, machined brass, riveted cage, injection-molded cage, crown cage, window cage, snap cage, or one-piece polymer design.
Pocket geometry deserves particular attention. The pocket must retain and guide the rolling element without creating interference across the expected operating range. An undersized pocket may restrict ball or roller movement. An oversized or poorly shaped pocket may permit excessive movement, poor guidance, or unstable cage motion. Pocket spacing errors can accumulate around the circumference and alter separator function even when an individual pocket appears acceptable.
Measurement methods should be matched to the tolerance and feature. Calipers are useful for broad checks but are not adequate for all critical cage features. Go/no-go gauges, air gauges, optical measurement systems, coordinate measuring machines, form gauges, profile projectors, and purpose-built functional fixtures may be more suitable. For flexible polymer cages, inspection conditions need control because temperature and moisture can affect measured dimensions. A dimensional result without the associated measurement method, gauge status, and environmental condition may not be meaningful.
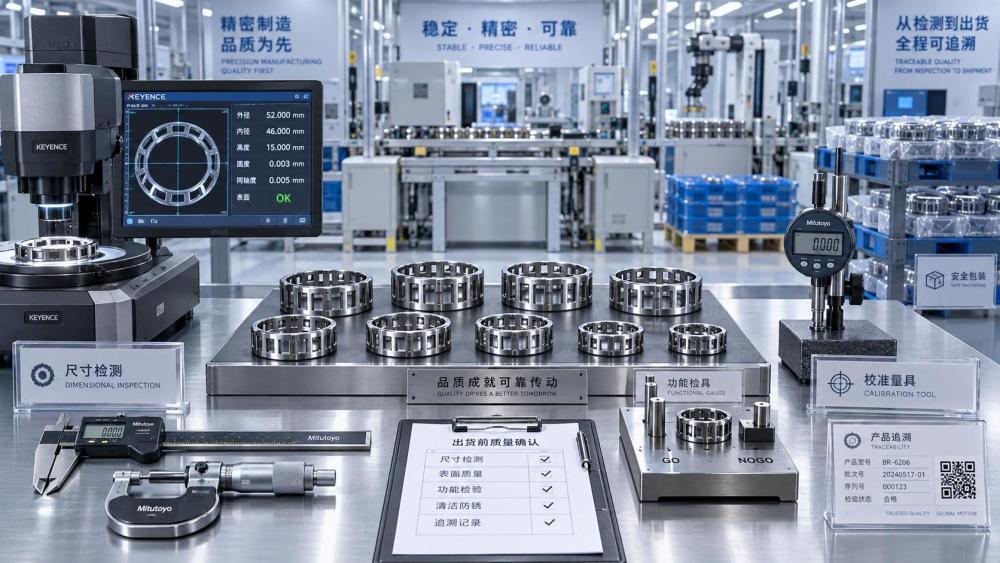
Functional gauges are especially important when a drawing dimension does not fully describe assembly behavior. A gauge that simulates the relevant rolling element, ring land, or assembly position can reveal pocket interference, snap-fit failure, incorrect rivet spacing, or distorted cage form that isolated measurements may miss. Gauge design must itself be controlled, calibrated, and protected from wear; an unverified functional gauge can create false acceptance across an entire lot.
Surface condition is a safety and reliability requirement
Sharp edges, stamping burrs, machining swarf, cracks, dents, tool marks, and loose particles can damage rolling elements or raceways after assembly. Such defects may also contaminate lubricant and accelerate wear. A bearing retainer factory should define visual acceptance criteria with sufficient specificity to distinguish harmless cosmetic variation from a feature that can affect function.
Edges created by stamping, piercing, broaching, machining, or trimming require controlled deburring. The objective is not simply to make the part feel smooth. Burr height, direction, attachment strength, and location matter. A burr facing a rolling path, a rivet interface, or a seal can detach in service or generate local interference. Deburring operations should not create secondary damage such as rounded critical forms, embedded media, excessive material removal, or deformation of thin bridges.
Crack inspection must be proportionate to the material, process, and application risk. Visual inspection can detect obvious forming cracks, incomplete rivets, and surface splits. Where the process or specification indicates elevated risk, suitable non-destructive methods may be required. Magnetic particle inspection can be relevant for ferromagnetic components; penetrant methods may be appropriate for certain nonporous metallic surfaces. The selected method, acceptance level, cleaning process, and inspector competence should be defined by the applicable specification rather than applied indiscriminately.
Surface finish requirements should be verified where the drawing specifies roughness, waviness, plating condition, or other surface characteristics. A low average roughness value alone does not guarantee a suitable surface. Deep directional scratches, folded material, drag marks, laps, or coating nodules can still create local failure points. Inspection must consider the actual contact and clearance zones of the cage.
Heat treatment, forming stability, and coating need objective verification
Not every bearing retainer is heat treated, but where heat treatment is specified, final shipment should be tied to the relevant thermal batch records and verification results. Depending on design, this can include hardness, case depth, microstructure, distortion, retained austenite limits, temper condition, or stress-relief confirmation. The required checks must come from the engineering specification; there is no single hardness range suitable for all cages.
Hardness testing should be performed on approved locations and with a method appropriate to part thickness and material condition. Testing a thin stamped cage with an unsuitable scale or excessive test load can produce misleading results or damage the part. For small components, microhardness testing or representative coupons may be specified. When coupons are used, their relationship to the actual production parts must be controlled; a coupon that did not experience the same thermal mass, loading arrangement, or furnace exposure may not represent the lot.
Forming and heat treatment can both create distortion. A cage that was dimensionally acceptable after stamping may become out-of-round after stress relief, coating, washing, or storage. Final geometry inspection should occur after the last process capable of changing the relevant feature. This principle also applies to plated or coated cages. Coating thickness, adhesion, coverage, corrosion-protection performance, and hydrogen-embrittlement control, where relevant to the material and process, should be addressed in the approved process plan.
Coating inspection should not be reduced to color comparison. Incomplete coverage, excessive build-up in pockets, poor adhesion, surface blistering, and contamination can affect fit and durability. If corrosion resistance is a customer requirement, the test method and acceptance criteria should be clearly referenced in the purchase specification. Generic claims that a coating is “rustproof” are not an acceptable release criterion.
Cleanliness control must consider the finished bearing environment
Cleanliness is one of the most frequently underestimated release controls. A cage can be dimensionally correct and visually acceptable while carrying abrasive particles, residual stamping oil, machining chips, wash chemical residues, blasting media, fibers, or loose coating fragments. Once enclosed in a bearing, these contaminants can enter rolling contacts and degrade lubricant performance.
The required cleanliness level should be defined by the bearing application and assembly process. Open industrial bearings assembled in a controlled plant may tolerate a different condition from precision bearings used in clean machinery, high-speed spindles, aerospace equipment, or sensitive hydraulic and electric-drive systems. The supplier and customer should agree on practical criteria: visual cleanliness, particle extraction and count, gravimetric residue, residual oil limits, packaging cleanliness, or other applicable methods.
Washing is effective only when the process is controlled. Dirty wash baths, exhausted filtration, inadequate drying, or unsuitable corrosion inhibitors can transfer rather than remove contamination. Final inspection should also confirm that no water spots, chemical staining, trapped media, or corrosion has developed after cleaning. Parts should be handled with clean gloves or controlled tools after final wash; otherwise, a validated cleaning process can be defeated at the packing station.
Sampling plans require risk-based boundaries
Sampling can be appropriate for stable, capable processes, but it should not be used to avoid controlling critical characteristics. A supplier should define which features are checked at start-up, during production, after tool change, after maintenance, after batch change, and at final release. Features with severe failure consequences may require 100% inspection, automated vision verification, functional gauging, or validated process monitoring rather than a small end-of-lot sample.
Acceptance sampling plans may be established using recognized statistical principles, including methods aligned with ISO 2859-1 when attribute sampling is contractually appropriate. However, an acceptable sampled lot does not prove that every unit is defect-free. The sampling level, inspection severity, lot size, defect classification, and response to rejection must be documented. Critical safety-related defects should not be treated in the same way as minor cosmetic deviations.
Process capability evidence can support reduced inspection only when the process remains under control. New tooling, worn punches, changed resin supply, furnace repair, revised lubrication, altered wash chemistry, or a new operator setup can all invalidate assumptions based on previous capability. Release authority should be able to require intensified verification when any of these changes occur.
Assembly verification can reveal defects hidden by component inspection
Where the retainer is supplied as part of an assembled bearing, final release should include checks that reflect the completed bearing arrangement. Cage freedom, rolling-element distribution, rivet security, rotation smoothness, abnormal noise, radial or axial clearance effects, and interference with seals or shields may need evaluation. A cage that passes its standalone drawing can still fail after assembly because of interaction with rings, rolling elements, rivets, or lubricant.
For separately supplied retainers, a controlled reference assembly or functional fixture remains valuable, particularly after tooling adjustments or process changes. The assembly method must not force the cage into position in a way that conceals an interference condition. Any destructive verification used for riveted, snap-fit, or molded features should be tied to defined lot controls and retained records.
Packaging is part of the conformity decision
Shipment damage can erase the value of rigorous manufacturing controls. Thin stamped cages may deform under stack load; machined cages can suffer impact damage; polymer cages may creep or distort under unsuitable temperature and compression; corrosion-sensitive materials may rust during transit if moisture protection is inadequate.
Packaging should prevent part-to-part abrasion, deformation, contamination, corrosion, and loss of lot identity. Dividers, trays, sealed clean bags, desiccants, vapor corrosion inhibitor materials, protective oil, and rigid outer cartons may be justified depending on material and route. Packaging materials must also be compatible with the part. For example, a protective oil or inhibitor should not leave residues that conflict with the customer’s lubricant, cleaning process, or polymer material.
Each package should carry enough information to preserve traceability through receiving: part number, revision where needed, quantity, manufacturing lot, inspection status, and shipment identifier. Final release should verify label accuracy against the physical contents. Wrong-label errors create a serious risk because they can place a technically conforming retainer into the wrong bearing family.
Standards support the system, but the drawing remains decisive
Quality management certification such as ISO 9001 can demonstrate that a factory operates a documented management system, but it does not by itself certify that a particular bearing retainer meets a specific drawing or application requirement. Likewise, bearing standards such as ISO 492 address dimensional tolerances for many radial bearing types, while ISO 15243 provides recognized terminology for bearing damage and failures. Neither should be assumed to replace the component-specific acceptance criteria agreed between supplier and customer.
The most defensible shipment decision is based on a controlled hierarchy: the purchase order, approved drawing, applicable customer specification, referenced material and process standards, validated inspection instructions, and retained objective evidence. A bearing retainer factory that can show this chain clearly is better positioned to prevent escapes, investigate field issues, and demonstrate that shipment release was based on functionally relevant controls rather than a final visual check alone.
Related News
- How to Assess a Rigid Coupling Supplier for Bore Accuracy and Traceable QualityOct 08, 2026Tribology & Kinematics Expert
- Titanium Alloys Compared: Balancing Strength, Corrosion Resistance, and MachinabilityOct 08, 2026CNC Kinematics Architect
- Where Ductile Iron Dismantling Joints Reduce Alignment Risk in Water PipelinesOct 08, 2026Pipeline Metallurgy Scientist
- Selecting a Precision Bearing Sleeve: Fits, Runout, and Material ChoicesOct 08, 2026Tribology & Kinematics Expert
- Face Milling Cutters: How Insert Geometry Affects Finish on Steel and AluminumOct 08, 2026CNC Kinematics Architect
- Single-Acting Cylinders for Clamping: Stroke, Force, and Return Spring ConsiderationsOct 07, 2026Fluid Power Control Strategist