
How to Vet a Steel Ingots Supplier for Grade Consistency and Delivery Risk
A low ingot price can become the most expensive part of a production order when the material arrives with variable chemistry, unclear heat identity, or a delivery date that does not match the melt shop schedule. When evaluating a steel ingots supplier, procurement teams should treat grade consistency and delivery performance as linked risks: poor production control creates quality interruptions, while weak planning and documentation make those interruptions harder to contain.
The practical objective is not to find a supplier that claims to produce the required grade. It is to establish whether that supplier can repeatedly deliver the same usable material condition, with traceable evidence, in the lot sizes and time windows your casting, forging, machining, or fabrication operation needs.
Start with the material requirement, not the supplier's grade label
A grade name alone is not a complete purchase specification. Two ingot lots described by the same commercial grade may perform differently if their chemical ranges, residual elements, deoxidation practice, melting route, cleanliness, or solidification condition vary. That difference can show up later as cracking during forging, inconsistent hardness after heat treatment, excessive machining-tool wear, porosity in cast products, or unstable mechanical properties in the finished part.
Before requesting quotations, convert the internal engineering requirement into a procurement specification that can be checked at receipt. The document does not need to be unnecessarily complex, but it should remove room for assumption. Include the required material designation and applicable standard where your organization has defined one, plus the chemistry limits that are critical to the intended process. State whether a standard range is acceptable or whether tighter internal control is needed for elements that affect your application.
Also define the usable ingot condition. This can include ingot shape and nominal mass range, surface condition, permitted crop practice, marking method, packaging, and whether material from different heats may be combined in one shipment. For high-consequence applications, distinguish clearly between a representative sample and the actual heat analysis for each supplied lot.
That level of clarity changes the supplier discussion. Instead of asking, “Can you supply this grade?”, ask, “Can you supply this grade within these chemistry and traceability requirements on every release?”
Check consistency through evidence from multiple heats
A single material certificate proves little about repeatability. A supplier may provide an acceptable certificate for a sample order while using broader process variation across normal production. Ask for certificates from several recent heats of the same or closely comparable grade, preferably across different production periods. The purpose is not to audit the supplier's entire operation; it is to see whether the reported chemistry is controlled near a predictable target or merely falls somewhere inside a wide allowable band.
Pay particular attention to elements that matter downstream. Carbon and alloying elements influence hardenability, strength, weldability, and heat-treatment response. Sulfur and phosphorus can be especially important where ductility, fatigue resistance, weld quality, or forging performance is sensitive. Residual elements may also matter when the material will undergo demanding forming, machining, or thermal processing.
A consistent supplier can explain its target chemistry, normal control approach, and what happens when a heat falls outside the agreed range. A vague response such as “all material meets standard” is not enough when your process depends on stable behavior rather than minimum compliance.
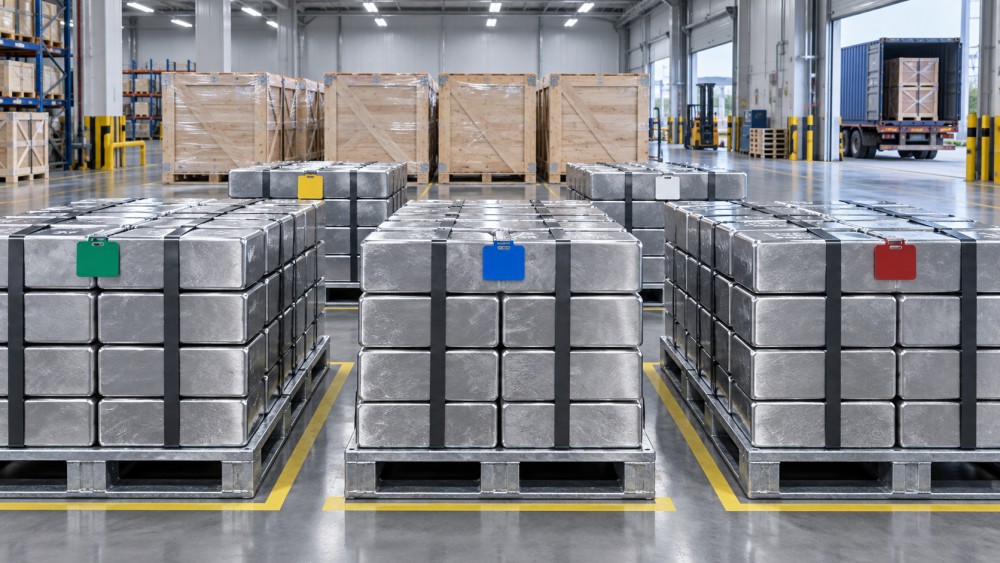
Review the identity chain as carefully as the chemistry. Each ingot, bundle, or packaged unit should remain connected to a heat number or lot number that appears on the material test certificate. If material is cut, repacked, stored, or consolidated before shipment, the supplier should be able to preserve that link. Once traceability is broken, a later nonconformance becomes expensive to isolate: the receiving team may need to hold an entire delivery rather than a defined heat.
What a useful quality package should contain
Documentation should support a receiving decision, not become paperwork that arrives after the material has already entered production. For each shipment, request a material test certificate that identifies the supplier, material grade, heat or batch number, chemical analysis, quantity, and shipment reference. The details must match the physical markings and commercial documents.
Depending on the application, the buyer may also need evidence of mechanical testing, inspection results, heat-treatment records, dimensional checks, or non-destructive examination. These are not universal requirements for every steel ingot purchase. Requiring every possible document can raise cost and slow supply without improving the decision. The right level of evidence depends on what the ingots will become.
Do not confuse a certificate template with a reliable quality system. Compare the certificate data with packing lists, markings, and received material. Repeated mismatches in dates, heat numbers, quantities, or analysis presentation are operational warning signs even when the nominal grade appears correct.
Audit the controls behind the certificate
Certificates matter because they reflect a process. The buyer should therefore understand, at a practical level, how the supplier makes and controls the ingots. This does not always require an on-site audit before an initial order, but it does require specific questions and credible answers.
- What melting and refining controls are used for the grades being quoted?
- How is chemical composition sampled, tested, and released?
- How are nonconforming heats identified, held, reworked, or rejected?
- What prevents different grades or heats from being mixed during storage and dispatch?
- How are ingots inspected for visible surface defects, damage, contamination, and marking legibility?
- Can the supplier provide a controlled sample order from the same production route planned for future supply?
The answers should be consistent with the supplier's claimed capability and order volume. A company may be a suitable source for common grades and short replenishment orders but not for tightly controlled chemistry, special melt practices, or critical production scheduling. That is not automatically a reason to reject the supplier. It is a reason to match the source to the risk level of the application.
For larger programs, involve quality and process engineering early. Procurement can evaluate commercial terms and supplier responsiveness, but engineers should confirm which chemistry limits, metallurgical attributes, and incoming checks are genuinely necessary. This prevents an avoidable conflict later, when purchasing has bought to a broad grade description but production needs a narrower operating window.
Delivery risk is more than quoted lead time
Quoted lead time is often treated as the delivery commitment. It is only one part of the risk. A reliable steel ingot source should be able to explain what inventory is genuinely available, what quantity requires new melting, which steps are capacity constrained, and when documents and material will be ready for dispatch.
Ask for the supplier's order-to-shipment sequence. The answer should separate stock material from made-to-order heats, quality release from physical production, and dispatch readiness from port departure or carrier collection. A shipment cannot support your production plan if it is physically ready but held for incomplete certificates, missing inspection approval, export documents, packaging rework, or a lack of booked transport.
For international sourcing, define the delivery point and handover responsibility in the purchase order. The procurement team should know who arranges loading, inland movement, export handling, freight booking, insurance where applicable, and document release. Ambiguous responsibility turns an ordinary logistics delay into a dispute over who must act.
Use a delivery-risk review before awarding volume
A supplier with a modestly higher unit price may be the lower total-cost option when it protects furnace scheduling, avoids emergency spot buying, and reduces the chance of production downtime. Compare quotations using a wider cost view:
- Material price and any surcharge mechanism
- Expected yield loss from ingot condition, cropping, or quality holds
- Cost of incoming inspection and document reconciliation
- Inventory required to absorb variability in supply
- Freight, packaging, handling, and claim exposure
- Cost of a delayed or rejected lot to the downstream production schedule
This does not mean every order needs the most conservative logistics plan. Standard, non-critical material may be purchased efficiently through scheduled releases and normal inventory buffers. A project tied to a fixed forging campaign, infrastructure package, or customer delivery date needs stronger controls: defined shipment windows, pre-dispatch document review, clear escalation contacts, and contingency sources where qualification risk justifies them.
Run a trial order that tests the real supply process
A small trial should test more than the ingot itself. Ask the supplier to process the order through the same route intended for regular business, including heat identification, certification, packaging, dispatch communication, and delivery. Receiving should verify the markings and quantities against documents before the material is released to production. Production should record relevant outcomes such as surface condition, melting behavior, forgeability, machinability, heat-treatment response, or defect rates, depending on the intended use.
One acceptable trial lot is a starting point, not proof of long-term consistency. The useful decision point comes after repeat deliveries show that quality records, physical condition, communication, and delivery execution remain stable. If a supplier changes melt source, production location, logistics route, or material control method, reassess the impact before treating the new arrangement as equivalent.
Common procurement mistakes that increase exposure
The most frequent error is buying against a general grade description while relying on engineering to solve material variation after receipt. Another is accepting certificates only after shipment, when the material may already be on the way to a time-sensitive operation. Procurement teams also sometimes qualify a supplier based on response speed and sample quality, without checking whether the supplier can reserve capacity and maintain lot traceability at program volume.
Price comparisons can be misleading when quotations do not use the same basis. One supplier may include testing, export packing, or delivery to a defined point while another excludes them. One may quote readily available stock, while another is quoting a future production heat. Put all bids on a common commercial and technical basis before ranking them.
Global Industrial Machining & Piping Equipment Network (IMPE) frames supplier evaluation around the connection between material performance, inspection capability, traceability, and downstream manufacturing outcomes. For buyers of ingots used in castings, forged parts, shafts, machined components, or industrial equipment, that connection is more useful than judging a supplier from a catalog alone.
Make the award conditional on measurable operating controls
The strongest purchase order is not the longest one. It is the one that makes acceptance, timing, and escalation clear enough that both sides can manage exceptions. Attach the approved material specification. State required certificates and heat marking. Define whether substitutions, mixed heats, partial shipments, or altered packaging require prior approval. Establish when shipping documents must be sent and what information the advance shipment notice must include.
For recurring supply, track each delivery against a concise supplier scorecard: conformance of chemistry and documents, traceability accuracy, shipment completeness, delivery performance against the agreed window, response to discrepancies, and effectiveness of corrective action. The scorecard should identify patterns, not merely record isolated complaints.
A capable supplier is not one that never encounters a problem. It is one that identifies the affected heat, provides usable evidence, communicates early, and prevents the same failure from recurring. That is the standard procurement teams should use when the material will influence the quality and schedule of every operation that follows.
Related News
- How to Assess a Rigid Coupling Supplier for Bore Accuracy and Traceable QualityOct 08, 2026Tribology & Kinematics Expert
- Titanium Alloys Compared: Balancing Strength, Corrosion Resistance, and MachinabilityOct 08, 2026CNC Kinematics Architect
- Where Ductile Iron Dismantling Joints Reduce Alignment Risk in Water PipelinesOct 08, 2026Pipeline Metallurgy Scientist
- Selecting a Precision Bearing Sleeve: Fits, Runout, and Material ChoicesOct 08, 2026Tribology & Kinematics Expert
- Face Milling Cutters: How Insert Geometry Affects Finish on Steel and AluminumOct 08, 2026CNC Kinematics Architect
- Single-Acting Cylinders for Clamping: Stroke, Force, and Return Spring ConsiderationsOct 07, 2026Fluid Power Control Strategist