
Forged Roll Price Benchmarks: What Drives Cost in Heavy-Duty Mill Roll Procurement?
A forged roll quotation can look straightforward until two suppliers price what appears to be the same roll and the gap is large enough to disrupt a maintenance budget or capital project estimate. In heavy-duty mills, the difference is rarely explained by steel weight alone. A lower-priced roll may exclude deep hardening, full ultrasonic inspection, final grinding, matching journal geometry, or the documentation needed to verify that the supplied roll matches the drawing.
For procurement teams, the useful way to assess forged roll price is to separate the cost of material, forging, heat treatment, machining, inspection, and commercial risk. The best benchmark is not a single price per kilogram. It is a normalized comparison of technically equivalent rolls, with each supplier’s scope, assumptions, and exclusions made visible before an order is placed.
Start by defining the roll that is actually being purchased
A mill roll is often described in early enquiries with only body diameter, face length, and material grade. That may be enough to obtain a rough budget figure, but it is not enough for a reliable comparison. The supplied part may include a working barrel, journals, shoulders, keyways, drive-end features, cooling passages, coatings, balancing requirements, and surface finish requirements. Each feature can change both manufacturing route and inspection effort.
Before treating any quotation as a benchmark, align the request around a controlled technical package. It should identify the roll function, operating loads, contact conditions, roll speed, expected temperature range, mating material, and whether the roll is intended for roughing, finishing, calendering, crushing, straightening, conveying, or another process. A forged backup roll and a forged work roll may have comparable outside dimensions yet need very different surface properties and internal quality levels.
- Finished barrel diameter, face length, overall length, and journal dimensions
- Required forging grade or approved material alternatives
- Target hardness range, effective hardened depth, and hardness test locations
- Surface roughness, crown profile, taper, runout, and concentricity limits
- Machining details such as keyways, threads, holes, grooves, or couplings
- Non-destructive testing requirements and acceptance criteria
- Material certification, heat-treatment records, dimensional reports, and marking requirements
- Preservation, packaging, transport orientation, and delivery point
This level of definition prevents a frequent procurement problem: one supplier prices a near-net forged blank while another prices a fully machined, tested, ready-to-install roll. The nominal unit prices cannot be meaningfully compared until the scope is equal.
Material grade sets the baseline, but chemistry is only part of the cost
Carbon steel rolls used under moderate load normally begin with a lower material cost than alloy steel rolls designed for wear resistance, high compressive stress, or cyclic thermal loading. Alloy additions can increase raw material expense, but the larger commercial impact often comes from process control. Higher-alloy grades may require tighter melting practice, more careful forging temperatures, controlled cooling, longer heat-treatment cycles, and additional verification before release.
Procurement should not assume that a familiar grade designation automatically means identical performance. Material standards may permit composition ranges, and mills may offer internal grades with different cleanliness or hardenability characteristics. The quotation should state the applicable specification, chemical analysis requirements, mechanical-property requirements, and whether the roll is made from ingot, billet, or a defined stock source.
For high-load service, steel cleanliness matters because internal inclusions and segregation can affect fatigue behavior and crack initiation. A supplier that prices cleaner feedstock, performs more reduction during forging, or applies more extensive ultrasonic examination may be more expensive for valid reasons. Conversely, a lower offer should prompt the question: which material and verification controls have been reduced?
Do not substitute hardness for grade verification
Hardness is a useful acceptance parameter, but it does not fully confirm chemical composition, microstructure, or core strength. Two rolls can show similar surface hardness while having different effective hardened depths or different resistance to spalling under load. When service conditions are demanding, require both the specified grade and the required hardness profile. This is particularly important when the barrel will be reground during its service life; shallow hardening can shorten the usable regrind allowance.
Size influences more than steel weight
Large diameter and long-face rolls are expensive not simply because they contain more metal. Their dimensions can determine the required forging press capacity, furnace size, quench handling, machine-tool envelope, grinding capacity, lifting arrangement, and transport method. A roll that sits near a supplier’s equipment limit usually carries additional scheduling and handling risk even when its mass is within the plant’s stated capacity.
Length-to-diameter ratio also matters. A long, slender roll can be more difficult to machine and grind while maintaining runout and crown requirements. Heavy journal transitions may need carefully controlled machining to avoid stress concentrations. When the drawing requests a very low runout tolerance across a long face, the supplier may need multiple setup checks, intermediate stress relief, or precision grinding passes. Those operations affect price and lead time.
Ask suppliers to state both forging weight and finished weight. The difference reveals how much stock is expected to be removed. Extra machining allowance may be appropriate for large forgings or difficult geometry, but an unusually high allowance can add cost through material waste, turning time, and heat-treatment distortion correction.
The forging route changes internal quality and cost exposure
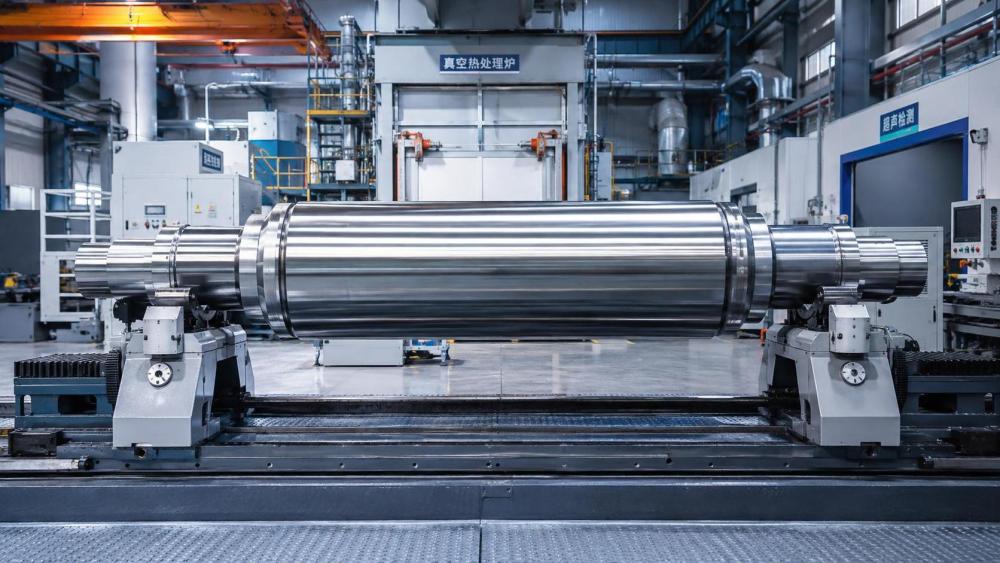
Forging is used to refine grain flow and reduce internal discontinuities in components that carry substantial loads. However, not all forged rolls undergo the same deformation history. Open-die forging may be suitable for many large custom rolls, while other designs may use more specialized forming routes. The key procurement question is whether the proposed process delivers adequate reduction, soundness, and grain orientation for the roll’s working stresses.
A quotation that merely says “forged steel” leaves several important issues unanswered. It does not state the starting stock, reduction ratio, whether the critical barrel and journal areas receive sufficient working, or how the supplier controls internal defects. This does not mean every order needs a detailed manufacturing procedure, but critical rolls should have a documented process route consistent with the drawing and service duty.
Where a supplier offers an alternative forging route, compare it against the acceptance requirements rather than rejecting or accepting it on terminology alone. The alternative may be technically suitable, but it should still meet the agreed material properties, non-destructive examination level, dimensional tolerances, and heat-treatment requirements. Lower cost is meaningful only when those outcomes remain equivalent.
Heat treatment is often the least visible line item and the most consequential one
Normalizing, quenching, tempering, stress relieving, induction hardening, and flame hardening can all appear in roll manufacturing, depending on grade and duty. Each method affects hardness distribution, residual stress, toughness, and distortion. The correct treatment is determined by the roll’s application, not by a generic preference for the highest hardness available.
A wear-facing roll may need a hard barrel with a tougher core and journals. A heavily loaded support roll may prioritize through-section strength and fatigue resistance over a very hard surface. Poorly controlled quenching can create cracking risk or excessive distortion; insufficient tempering can leave the roll vulnerable to brittle damage. Correcting distortion after heat treatment may require additional machining and grinding, which explains part of the variation in a forged roll price.
Review heat treatment in terms of deliverables. A technically complete quotation should clarify whether it includes furnace records, hardness mapping, test coupons where applicable, stress relief after rough machining, and final verification after finish grinding. If the buyer only requests “heat treated,” suppliers may make different assumptions, producing quotations that look comparable but are not.
Machining precision can outweigh a modest difference in material cost
Heavy rolls often require extensive turning before and after heat treatment, followed by finish grinding of the barrel and journals. The barrel may require a defined crown to compensate for deflection or process loading. The journals must fit bearings, chocks, couplings, or drive assemblies without introducing alignment problems. A small error in journal diameter, shoulder location, or runout can create installation delays far more costly than the original purchase saving.
When reviewing bids, distinguish between general machining tolerances and the tolerances that control roll performance. Barrel cylindricity, total indicated runout, journal concentricity, face profile, surface roughness, and transition radii deserve explicit attention. Also verify the datum scheme. A supplier may inspect dimensions from a different reference surface than the one used by the mill’s assembly drawing, which can create disagreement after delivery.
Surface condition should be described in practical terms. A ground finish is not automatically sufficient where the process requires a specified roughness direction, a polished contact surface, or a textured barrel. If a coating, rubber covering, or later surface treatment will be applied, confirm the required pre-treatment finish and any masking around journals or shoulders.
Testing requirements should be priced as scope, not treated as an optional afterthought
For critical rotating components, inspection is part of the product definition. Ultrasonic testing can identify internal discontinuities; magnetic particle examination can help detect surface and near-surface indications in ferromagnetic materials; dimensional inspection confirms that the roll can be installed as intended. The cost depends on roll size, test coverage, test stage, acceptance threshold, and reporting requirements.
Specify whether examination is needed after forging, after rough machining, after heat treatment, or at final condition. Testing after rough machining may provide better access to the relevant surface than testing on heavy scale. Final testing may be necessary after grinding or machining has removed material. Requiring both can be justified for severe duty, but should be deliberate rather than copied from an unrelated specification.
Documentation requests should match the consequence of failure. A spare roll for a low-speed auxiliary line may not need the same report package as a primary production roll whose unplanned failure stops a major process. The goal is neither minimum paperwork nor maximum paperwork; it is evidence proportionate to operational risk.
How to compare quotations without rewarding hidden exclusions
Build a comparison sheet that uses one technical baseline and separates mandatory scope from alternatives. Avoid ranking suppliers by total price before identifying whether all offers include the same finished condition. A supplier may quote competitively because it assumes the buyer will provide final grinding dimensions later, accepts a wider hardness range, omits special packaging, or does not include a third-party witness requirement.
- Freeze the commercial comparison basis. Use the same revision-controlled drawing, specification, quantity, delivery location, and requested documentation list for every bidder.
- Ask for a scope breakdown. Material, forging, heat treatment, rough machining, finish machining, grinding, testing, documentation, packaging, and freight should be identified even if suppliers do not disclose internal cost margins.
- List deviations separately. Do not let an alternative grade, altered hardness range, omitted test, or changed delivery term disappear inside a lower total.
- Review manufacturing capacity against the part envelope. Confirm that the supplier can forge, heat treat, machine, grind, inspect, and handle the roll internally or has a controlled subcontracting plan.
- Evaluate delivery as a production sequence. Lead time should account for material procurement, forging slots, heat-treatment availability, machining, inspection, report review, and transport preparation.
This approach also improves negotiation. Instead of requesting an unexplained discount, the buyer can identify a specific cost driver: perhaps a less demanding surface finish is acceptable, perhaps testing can be aligned with a realistic risk level, or perhaps several similar rolls can be scheduled together to reduce setup and handling costs. These are defensible commercial discussions because they preserve visibility over technical trade-offs.
When a low bid deserves additional scrutiny
A low bid is not automatically a quality problem, but it should trigger targeted questions when it differs sharply from comparable offers. Check whether the supplier has quoted finished dimensions or a forging blank, whether the stated material is truly equivalent, and whether final inspection reports are included. Examine hardening depth, not just surface hardness. Confirm that the barrel can be reground without falling below the required property zone.
Also ask who is responsible if the roll fails incoming inspection because of runout, dimensional error, or test indications. The answer should cover disposition, replacement, rework authorization, transport responsibility, and report traceability. Vague terms such as “subject to final confirmation” can be reasonable during an early budget stage, but they should be resolved before a purchase order is released.
Freight and preservation are another source of misleading comparisons. A large forged roll may need corrosion protection, protected journal surfaces, purpose-built supports, and handling instructions to avoid damage in transit. A price that excludes suitable packing can move cost and risk to the receiving site.
Use lifecycle value when the roll affects mill availability
The purchase price is most important when several technically compliant options are available. Yet for rolls that influence line availability, consider the cost of early regrinding, bearing damage from poor journal geometry, unplanned replacement, and lost production time. A roll with verified material quality, stable heat treatment, accurate grinding, and complete inspection records may justify a higher initial cost when it reduces uncertainty in a high-consequence position.
That does not require accepting every premium feature offered by a supplier. It requires matching the specification to service duty and making every quote answer the same technical question. Once material condition, forging route, heat treatment, finished geometry, testing, documentation, delivery scope, and deviation list are aligned, the forged roll price becomes a usable procurement benchmark rather than a number that conceals different products.
Related News
- How to Assess a Rigid Coupling Supplier for Bore Accuracy and Traceable QualityOct 08, 2026Tribology & Kinematics Expert
- Titanium Alloys Compared: Balancing Strength, Corrosion Resistance, and MachinabilityOct 08, 2026CNC Kinematics Architect
- Where Ductile Iron Dismantling Joints Reduce Alignment Risk in Water PipelinesOct 08, 2026Pipeline Metallurgy Scientist
- Selecting a Precision Bearing Sleeve: Fits, Runout, and Material ChoicesOct 08, 2026Tribology & Kinematics Expert
- Face Milling Cutters: How Insert Geometry Affects Finish on Steel and AluminumOct 08, 2026CNC Kinematics Architect
- Single-Acting Cylinders for Clamping: Stroke, Force, and Return Spring ConsiderationsOct 07, 2026Fluid Power Control Strategist