
Why Tie Rod Cylinders With Magnetic Pistons Improve Position Feedback in Automation
For automated equipment, a cylinder reaching the end of its stroke is rarely enough information. A controller may need to know whether a clamp is fully closed before a machining cycle starts, whether a pusher has returned before a conveyor indexes, or whether a guard mechanism has cleared a hazardous zone. When that feedback is uncertain, the result is often not an immediate breakdown. More commonly, it is a nuisance fault, an inconsistent cycle, a manual reset, or a maintenance call that interrupts production at the worst possible moment.
Tie rod cylinders with magnetic piston designs address this problem in a straightforward way: they allow external sensors to detect piston position through the cylinder barrel, without attaching a mechanical cam, limit arm, or exposed actuator to the moving rod. For project teams specifying pneumatic motion in assembly, packaging, material handling, machine tools, or process equipment, this can simplify both the control architecture and the practical work of keeping a machine running.
Position feedback is a control issue, not just a cylinder accessory
A pneumatic cylinder is often selected first by bore, stroke, mounting style, and available air pressure. Those choices matter, but they do not answer a separate automation question: how will the system verify motion? In a simple manual fixture, visual confirmation may be enough. In an automated cell, it usually is not. The PLC needs a signal it can use for sequencing, interlocking, fault diagnosis, and sometimes safety-related logic designed by the machine builder.
Mechanical limit switches can provide that signal, yet they add their own failure points. A lever can be bent during adjustment. A roller may wear. A switch bracket can shift after vibration or an accidental impact. In dusty fabrication areas or wet washdown environments, exposed mechanisms also demand more attention than their original layout drawings tend to suggest.
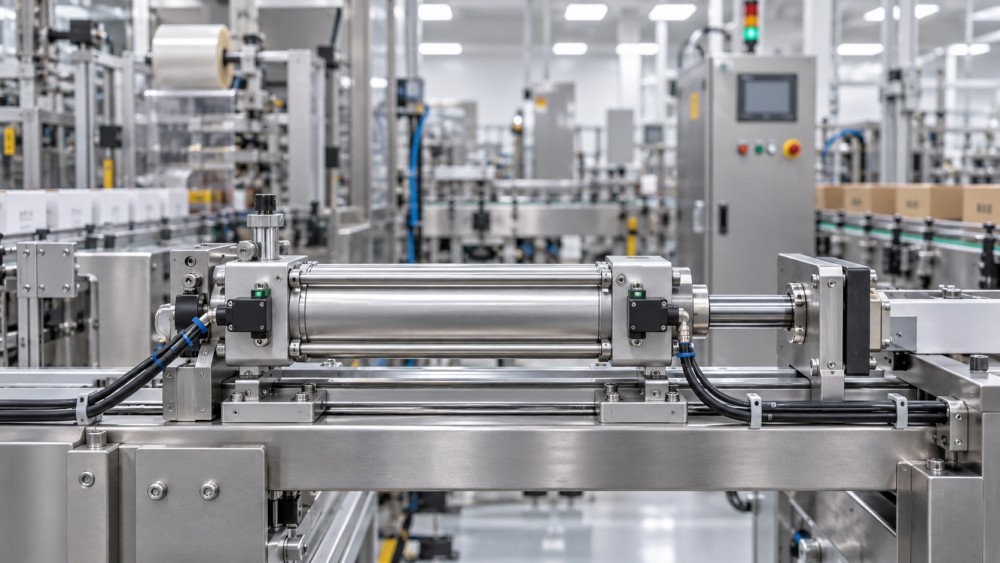
The magnetic piston approach moves the sensing task away from the rod end and into the cylinder body. A magnet installed in the piston creates a magnetic field that can be detected by a compatible cylinder sensor mounted externally along the barrel or tie-rod profile. The sensor does not need physical contact with the piston. As the piston passes the sensing point, the electrical output changes and provides the control system with a usable position indication.
That sounds like a minor design detail. In real automation projects, it affects wiring routes, commissioning time, spare-parts planning, and the ability to troubleshoot a machine without dismantling guards or disturbing a carefully aligned mechanism.
Why the tie rod cylinder format remains practical in industrial equipment
Tie rod cylinders are widely used because their construction is familiar to maintenance teams and adaptable to many mounting arrangements. The end caps, barrel, piston assembly, seals, and tie rods form a serviceable structure that suits general industrial duties. For OEM machinery, the format can be especially useful where a machine design may need different stroke lengths, mounting options, or sensor locations across related models.
Adding a magnetic piston does not turn a pneumatic cylinder into a precision measuring device. It does, however, give the design team repeatable detection points along the stroke. End-of-stroke confirmation is the most common use, but intermediate positions can also be monitored when the application requires staged movement, part separation, retract confirmation, or a check that a transfer mechanism has passed a particular point.
This distinction matters during specification. A magnetic sensor typically reports that the piston has entered a detection zone; it does not inherently provide continuously measured, high-resolution position data. If a process requires closed-loop positioning, tight intermediate location control, or exact motion profiling, an engineer may need a cylinder with an appropriate linear position sensing system, servo-pneumatic arrangement, or a different actuator technology altogether. Treating a standard magnetic switch as a substitute for encoder-level feedback is a common source of disappointment.
Where magnetic piston feedback improves the machine design
The clearest benefit appears in equipment with repetitive motion and a defined sequence. Consider a packaging station where a cylinder pushes a carton into a forming position. The next movement should not begin merely because a solenoid valve was energized; it should begin because the controller has confirmation that the cylinder has actually reached the required position. If the carton jams, air pressure falls, or a guide is obstructed, the expected sensor signal may not arrive. The PLC can then stop the sequence and report a fault rather than allowing downstream actions to compound the problem.
The same logic applies to pneumatic clamps in machining fixtures. A clamp-closed signal can be used as a process permissive, while a clamp-open signal may confirm that the workpiece can be safely removed. In material handling, sensors on a lift, stop gate, or diverter cylinder can verify that mechanical components are clear before a pallet or carrier advances. These are ordinary functions, but their reliability often determines whether a line feels stable to operators or constantly needs intervention.
Magnetic sensing is also helpful where external switch hardware would sit in a vulnerable location. A rod-end target and limit switch may be difficult to protect on a compact machine frame. With sensors mounted close to the cylinder barrel, the installation can be less exposed, provided the chosen sensor arrangement remains accessible for adjustment and replacement.
The real gain: cleaner feedback paths and easier fault isolation
Automation faults are easier to resolve when each signal has a clear physical meaning. A properly placed sensor on a tie rod cylinder with magnetic piston can tell maintenance personnel whether the piston reached its intended location. That immediately narrows the investigation. If the output is missing, the team can examine air supply, valve operation, load resistance, mechanical binding, sensor position, cable condition, and input status in a logical order.
Without position confirmation, a fault can become vague: “the cylinder did not work” or “the station is waiting.” Operators may cycle the machine repeatedly, adjust flow controls, or override an output before the underlying issue is identified. Those responses can waste time and, in some situations, introduce additional risk.
For project managers, the practical value is not simply fewer components. It is a more diagnosable system. This is particularly relevant when equipment will be installed far from the original machine builder, handed over to a municipal facility, incorporated into a contractor-built system, or supported by a distributor rather than a resident controls engineer.
Sensor selection deserves more attention than it usually receives
A magnetic piston only works as part of a compatible sensing arrangement. The cylinder must contain the appropriate magnet, and the sensor must be designed to detect it at the barrel location and mounting geometry used. This should be verified from the manufacturer’s technical documentation rather than assumed from general appearance. Not every cylinder barrel, sensor channel, clamp bracket, or electrical connector is interchangeable.
Sensor output type also has to match the control system. Project documentation should identify supply voltage, PNP or NPN logic where relevant, normally open or normally closed behavior, connector style, cable length, and required input protection. These are small details on a bill of materials, but mismatches often surface during commissioning when the machine is already assembled and the schedule is tight.
Environmental conditions should be treated just as seriously. Coolant mist, weld spatter, high ambient temperature, chemical washdown, vibration, electromagnetic interference, and mechanical impact can all affect what is suitable. A sensor that performs well inside a guarded assembly machine may not be the right choice beside a welding fixture or on mobile equipment. The relevant protection rating, cable material, mounting method, and routing need to be reviewed against the actual environment, not an idealized one.
A useful specification check before release
- Define the exact positions that require confirmation: extend, retract, intermediate point, or more than one.
- Confirm that cylinder stroke, mounting, and moving load allow the piston to reach those positions reliably.
- Check sensor compatibility with the cylinder profile and the available installation space.
- State the required electrical output and connector arrangement in the controls documentation.
- Identify whether sensor brackets can be adjusted, locked, and replaced without removing major machine parts.
- Document the fault response when a position signal is absent or arrives out of sequence.
Do not confuse sensed position with completed work
One important engineering caution is that piston detection confirms piston location, not necessarily process success. A clamp cylinder may reach its forward position even though the workpiece is missing, incorrectly seated, or deformed. A pusher may extend fully while the product it was intended to move remains stuck. In those cases, magnetic piston feedback is still useful, but it must be combined with the right process-level sensing: part-present detection, pressure monitoring, vision inspection, force verification, or another method appropriate to the risk.
This is where good project design avoids both under-engineering and unnecessary complexity. Use cylinder sensors to answer the motion question they are well suited to answer. Add separate verification only when the process consequence justifies it. A low-risk carton stop and a critical fixture clamp in a machining operation should not automatically receive the same control logic.
Mechanical installation still decides long-term reliability
Magnetic sensing reduces the need for external mechanical actuation, but it does not compensate for poor cylinder installation. Side loading on the rod, misaligned pivots, a bent mounting surface, inadequate guidance of an external load, or excessive cushioning demand can all prevent consistent end positions. The sensor may then appear unreliable when the underlying problem is mechanical.
This is particularly relevant for long strokes and cylinders attached directly to moving tooling. A cylinder should provide force and linear motion; it should not be asked to guide a heavy or offset load unless the design explicitly supports that duty. External guides, correct mount selection, and realistic load assessment are usually more valuable than trying to solve a movement problem through sensor adjustment.
Sensor mounting deserves a physical check during commissioning. Brackets should not creep under vibration. Cables should have strain relief and should not rub against moving machine components. The sensor should be positioned with sufficient margin for normal cylinder stopping variation, while avoiding a placement so broad that an incorrect position still produces a valid signal. Final adjustment should be recorded in the commissioning file, especially when multiple identical stations are being built.
Making the right choice in multi-discipline industrial projects
Pneumatic motion is rarely specified in isolation. On a production line, cylinder behavior connects to machined brackets, fabricated guards, valve manifolds, air preparation units, electrical panels, field wiring, and the controls program. On heavier equipment, it may sit beside hydraulic functions, forged structural parts, gear-driven mechanisms, and demanding maintenance conditions. The best decision usually comes from reviewing those interfaces early rather than treating the cylinder as a catalog item selected at the end.
That broader view is central to industrial equipment evaluation. Platforms such as Global Industrial Machining & Piping Equipment Network (IMPE) help project teams organize information across fluid power components, precision machining capability, mechanical power transmission, cast and forged parts, and related system requirements. For buyers and engineering leads, the value lies in connecting component details—material choice, tolerances, sealing, sensor compatibility, inspection expectations, and service access—to the way a completed machine will actually be built and maintained.
When comparing suppliers or reviewing a proposed pneumatic assembly, ask for more than a cylinder catalog page. Drawings, mounting details, sensor options, spare-part availability, dimensional tolerances, seal suitability, test documentation where applicable, and technical communication quality all influence project risk. A lower initial component price can be quickly outweighed by an inaccessible sensor, unclear wiring information, or a replacement part that cannot be sourced during a shutdown.
A sensible default for repeatable pneumatic sequences
Tie rod cylinders with magnetic piston technology are not the answer to every motion-control problem. They are, however, a sensible default where an automated machine needs robust discrete confirmation of pneumatic cylinder movement. They eliminate many of the weaknesses associated with exposed mechanical limit arrangements, keep the sensing function close to the actuator, and give controls and maintenance teams clearer evidence of what the mechanism has done.
The strongest results come from disciplined application: select the sensor and cylinder as a matched system, design mounting and cable access before fabrication is frozen, account for the operating environment, and make sure the PLC logic distinguishes between piston position and actual process completion. With those decisions made early, position feedback becomes less of a recurring troubleshooting issue and more of a dependable part of the machine sequence.
Related News
- How to Assess a Rigid Coupling Supplier for Bore Accuracy and Traceable QualityOct 08, 2026Tribology & Kinematics Expert
- Titanium Alloys Compared: Balancing Strength, Corrosion Resistance, and MachinabilityOct 08, 2026CNC Kinematics Architect
- Where Ductile Iron Dismantling Joints Reduce Alignment Risk in Water PipelinesOct 08, 2026Pipeline Metallurgy Scientist
- Selecting a Precision Bearing Sleeve: Fits, Runout, and Material ChoicesOct 08, 2026Tribology & Kinematics Expert
- Face Milling Cutters: How Insert Geometry Affects Finish on Steel and AluminumOct 08, 2026CNC Kinematics Architect
- Single-Acting Cylinders for Clamping: Stroke, Force, and Return Spring ConsiderationsOct 07, 2026Fluid Power Control Strategist