
Vacuum Generators with Blow-Off Function: Sizing for Fast Pick-and-Place Cycles
Vacuum Generators with Blow-Off Function: Sizing for Fast Pick-and-Place Cycles
Vacuum generators with blow-off function are often selected for a simple reason: a robot, gantry, or pneumatic handling unit must pick a part securely and release it without hesitation. Yet high-speed pick-and-place performance is rarely determined by one catalog value. A generator may provide adequate ultimate vacuum and still miss parts, delay release, consume excessive compressed air, or become unstable when surface conditions change.
For technical evaluators, the sizing question is therefore not “Which ejector has the highest vacuum flow?” It is “Which vacuum source, cup arrangement, control sequence, and air supply condition will establish sufficient holding force within the available pick window, tolerate realistic leakage, and vent the system quickly enough for the next motion?” Blow-off capability belongs in that same calculation. It is not merely an accessory for dropping a product; it can determine whether a cell reaches its intended cycle time.
This matters across packaging, assembly, sheet handling, machining automation, electronics, plastics, food-related equipment, and metalworking. A stamped component with an oily surface, a porous corrugated carton, a thin film sheet, and a machined aluminum housing may all be handled by vacuum, but they create very different demands on the pneumatic circuit.
What Blow-Off Actually Changes in a Vacuum Handling Cycle
A pneumatic vacuum generator uses compressed air through a nozzle and venturi arrangement to create suction. When the vacuum valve is switched off, residual vacuum may remain in the cup, tubing, manifold, and any internal volume of the generator. On a fast-moving machine, that residual vacuum can make a lightweight part cling to the cup after the robot has reached the release position. The result can be poor placement accuracy, double stacking, dragged products, or a delay that forces a longer dwell time.
A blow-off function introduces a controlled pulse of positive pressure into the vacuum line or cup circuit. The pulse breaks the vacuum seal and helps separate the workpiece from the gripping surface. The objective is not maximum positive pressure for its own sake. Excessive blow-off can displace delicate parts, disturb adjacent products, create noise, or push contaminants toward the workpiece. It should be sufficient to make release repeatable under the least favorable expected conditions.
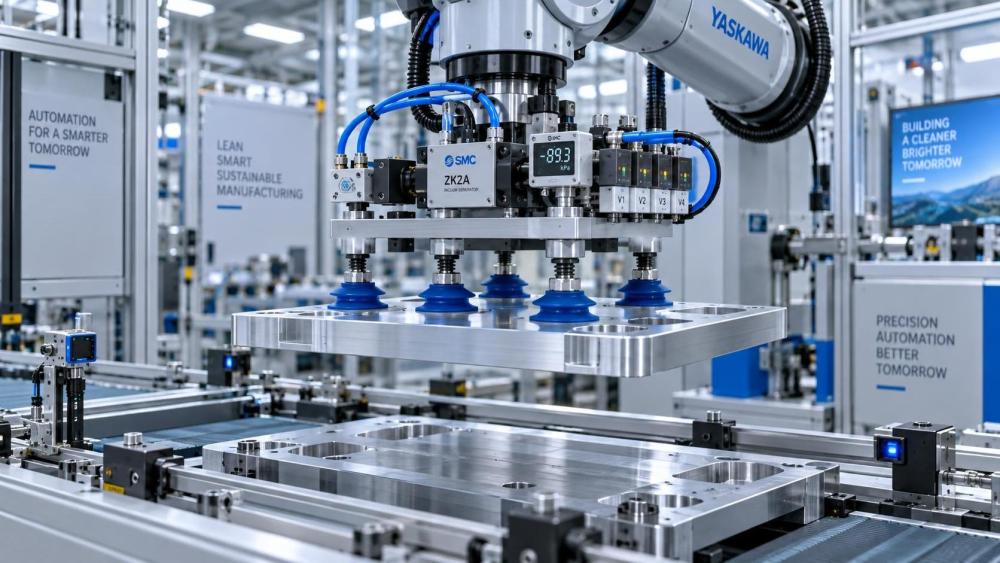
The practical implication is that vacuum generation and release cannot be sized independently. A larger vacuum volume may help stabilize gripping in one application, but it also takes longer to evacuate and vent. Longer or wider hoses may be convenient mechanically, but they increase the volume that must be managed during every cycle. A fast ejector mounted close to the cup can outperform a nominally larger centralized unit simply because the pneumatic path is shorter.
Start with the Part, Not the Generator Catalog
The workpiece defines the grip requirement. Weight is only one part of it. The vacuum holding force available at a cup is broadly related to the pressure difference across the cup and its effective sealing area. In simplified form, holding force is the pressure differential multiplied by the effective cup area. Real applications require a safety margin because acceleration, deceleration, robot orientation, vibration, cup deformation, surface contamination, and leakage all reduce usable margin.
A vertical lift of a rigid, flat part is usually the easiest condition. Horizontal transfer can introduce shear forces, especially during rapid acceleration. Handling a part below the gripper, rotating it, or stopping abruptly creates additional dynamic loading. Thin sheet materials create another challenge: the cup may pull the sheet upward, distort it, or lose its seal at an edge. For these jobs, cup geometry, cup count, spacing, and mechanical support may be as important as the vacuum generator itself.
Surface quality changes the sizing approach. Smooth glass, sealed plastic, and machined nonporous metal can reach vacuum quickly with relatively modest flow once the cup seals. Cardboard, textured molded parts, wood, fabric, foam, and rough cast surfaces leak continuously. These applications often demand higher suction flow to maintain vacuum, rather than simply a higher ultimate vacuum rating. Selecting a generator solely by its peak vacuum figure is a common error when the target material is porous or irregular.
The Parameters That Determine Generator Size
A useful sizing review brings several parameters into one application sheet. The values should be measured or estimated from the actual gripper layout where possible, rather than taken from a conceptual machine drawing.
- Required holding force: Include workpiece mass, orientation, acceleration, expected friction or shear loading, and a sensible safety allowance.
- Cup type and effective area: Diameter alone is not enough. Bellows cups, deep cups, foam pads, and lip profiles behave differently on uneven surfaces.
- Vacuum level at the cup: The relevant value is the pressure achieved at the cup under operating leakage, not the no-flow figure shown for an ejector.
- Evacuated volume: Include cup volume, manifolds, fittings, sensors, and hose internal volume. Long lines can dominate this value.
- Leakage rate: Consider porosity, surface grooves, imperfect seating, and the possibility that one cup in a multi-cup tool may not seal.
- Available pick and release time: Divide the motion sequence into actual milliseconds available for vacuum build, grip confirmation, transfer, blow-off, and part-clear verification.
- Compressed-air condition: Supply pressure, pressure stability, air cleanliness, and flow capacity at peak demand all affect ejector behavior.
Most manufacturers publish performance curves showing suction flow versus vacuum level at specified supply pressures. These curves are more useful than a single headline rating. A technical evaluation should compare the application’s estimated leakage and required vacuum against the curve at the actual regulated supply pressure. If the site pressure falls during simultaneous machine functions, a unit selected at ideal laboratory pressure may not deliver the intended pick response.
Fast Cycles Depend on Evacuation and Venting Time
The speed of vacuum build depends on the ratio between available suction flow and the volume being evacuated, while leakage continually works against the system. In a sealed application, a larger generator generally reduces pull-down time. In a leaking application, more flow may be needed merely to reach and maintain an acceptable operating vacuum. The control target should be the time to reach a usable gripping threshold, not the time to reach theoretical maximum vacuum.
Release follows a similar principle. The system must bring the cup circuit from negative pressure toward atmospheric pressure, and often slightly positive pressure, quickly enough for the workpiece to detach. A short, well-directed blow-off pulse can be effective when the cup has a good seal and the workpiece is light. A more difficult part, such as a thin plastic tray with static attraction or a part with a broad, compliant sealing surface, may need a different cup material, an adjustable blow-off restrictor, or a longer release window. Adding pressure blindly is rarely the most robust answer.
Some systems benefit from separating the vacuum and blow-off paths with suitable valves and restrictions so that release can be tuned without disrupting the vacuum-generation setting. Integrated generators can reduce external plumbing, while modular valve-and-ejector assemblies may offer more flexibility in larger tools. The preferred arrangement depends on how many cups are used, how close equipment can be installed to the end effector, and whether different zones need independent control.
Centralized or Decentralized Vacuum Generation?
This decision has a direct effect on cycle behavior. A centralized generator or vacuum pump can support multiple cups through a manifold. It may simplify maintenance and concentrate exhaust treatment in one location. However, long vacuum lines add volume and can slow both pick and release. They also make it harder to identify which cup or zone is leaking.
Decentralized vacuum generators mounted near individual cups or small cup groups reduce line volume and can improve response time. They are particularly useful for robotic end effectors with independent pick zones, mixed product formats, or high-speed indexing. The trade-off is more components at the tool, possible weight limits on the robot wrist, and a greater need to manage electrical connections, valves, exhaust air, and service access.
Do Not Ignore Air Consumption and Exhaust Conditions
Ejector-based vacuum is responsive and compact, but compressed air is not free. A generator that is oversized for a continuous or high-duty-cycle application can impose a material operating cost and create avoidable compressor demand. The right evaluation compares air consumption over the real duty cycle, including vacuum-on duration, blow-off pulses, simultaneous stations, and idle behavior. Vacuum-saving functions, check valves, pressure switches, and controlled on-demand operation may reduce consumption where the application allows them.
Exhaust air also deserves attention. In clean assembly areas, exhaust flow can stir dust or create objectionable noise. In machining cells, mist, coolant vapor, chips, and fine particles can affect cups, filters, valves, and sensors. Air preparation should be matched to the component supplier’s requirements, and filtration must be serviceable rather than hidden inside an inaccessible machine enclosure. Where oily or dusty workpieces are unavoidable, a trial with representative parts is more valuable than assuming a clean-room performance curve will translate directly.
Control Logic Is Part of Sizing
A well-sized generator can still perform poorly with weak sequence logic. The machine should distinguish between “vacuum command issued” and “part safely gripped.” A vacuum sensor, where appropriate, can confirm that the selected threshold has been reached before a high-speed transfer begins. For porous materials, the threshold and confirmation delay must account for normal leakage; otherwise, the control system may generate nuisance faults.
At release, the controller should coordinate blow-off duration with the end effector’s position and subsequent motion. If the robot starts retracting before part separation is complete, the product can be pulled out of position. If blow-off remains active too long, air use and part disturbance rise. Adjustable timing is useful, but the better goal is a repeatable release supported by a suitably low-volume circuit and a cup that suits the surface.
For machine builders, the same thinking applies to pneumatic valves, manifolds, sensors, tubing, and fittings. Restrictive components upstream of the ejector can reduce available flow. Restriction on the vacuum side can make a high-capacity generator appear slow. The circuit should be reviewed as a complete system rather than a list of individually acceptable components.
A Practical Evaluation Path Before Release to Production
Before finalizing vacuum generators with blow-off function, document the heaviest and lightest workpieces, surface variations, expected leakage, pick orientation, acceleration profile, cup arrangement, available supply pressure, and target cycle sequence. Ask suppliers for performance curves at the intended operating pressure and clarify whether stated flow values refer to free air, a particular vacuum point, or another test condition. Confirm the blow-off arrangement, its adjustment range, and whether it is integrated or requires external valving.
Then validate the design with representative parts, including the least favorable surfaces likely to appear in production. Measure vacuum build time at the cup, not only at the generator port. Observe release after repeated cycles, after line pressure variation, and when one cup does not seal as expected. This is also the time to assess noise, contamination exposure, hose routing, and maintenance access.
IMPE approaches hydraulic and pneumatic equipment selection through this wider system lens: component ratings matter, but so do material behavior, motion conditions, production tolerances, inspection needs, and long-term serviceability. For procurement and engineering teams, a clear requirement sheet makes supplier comparisons more meaningful and prevents a low initial component price from becoming a commissioning problem.
The strongest selection is usually not the generator with the largest published capacity. It is the one that reaches the required grip threshold in the available time, holds the real part with adequate margin, releases cleanly with a controlled blow-off pulse, and does so without placing unnecessary demand on the plant air system. Those criteria should be confirmed before the cycle-time commitment is locked into the machine design.
Related News
- How to Assess a Rigid Coupling Supplier for Bore Accuracy and Traceable QualityOct 08, 2026Tribology & Kinematics Expert
- Titanium Alloys Compared: Balancing Strength, Corrosion Resistance, and MachinabilityOct 08, 2026CNC Kinematics Architect
- Where Ductile Iron Dismantling Joints Reduce Alignment Risk in Water PipelinesOct 08, 2026Pipeline Metallurgy Scientist
- Selecting a Precision Bearing Sleeve: Fits, Runout, and Material ChoicesOct 08, 2026Tribology & Kinematics Expert
- Face Milling Cutters: How Insert Geometry Affects Finish on Steel and AluminumOct 08, 2026CNC Kinematics Architect
- Single-Acting Cylinders for Clamping: Stroke, Force, and Return Spring ConsiderationsOct 07, 2026Fluid Power Control Strategist