
Pneumatic Solenoid Valves Explained: Voltage, Porting, and Response Time
A pneumatic valve can be electrically correct and still be wrong for the machine. A coil may match the control supply, yet the valve may exhaust through the wrong path, restrict cylinder speed, or switch too slowly for the required sequence. That is why evaluating Pneumatic Solenoid Valves starts with the air circuit and motion requirement, then works back to voltage, porting, flow, and environmental conditions.
The solenoid does not create useful pneumatic motion by itself. It shifts a poppet, spool, or pilot stage that directs compressed air to an actuator. The resulting cylinder behavior depends on the entire system: supply pressure, tubing length, fitting bore, valve flow capacity, load, cylinder size, exhaust arrangement, and contamination level. A catalog comparison that focuses only on coil voltage or valve body size can miss the factors that determine cycle performance and reliability.
Start with the required valve function
Before selecting a coil or comparing response-time figures, define what the valve must do when it is energized and when power is removed. The basic question is whether the valve controls a single air path, reverses a double-acting actuator, or enables and disables an air supply to a larger circuit.
Common descriptions such as 2/2, 3/2, and 5/2 identify the number of ports and switching positions. The first number refers to ports; the second refers to positions. This notation is useful, but it does not replace reading the pneumatic symbol. Port labels, normal state, internal pilot arrangement, and exhaust routing still need to match the circuit drawing.
A frequent mistake is treating a 5/2 valve as interchangeable with any other 5/2 valve. A single-solenoid, spring-return version returns to its default state when power is lost. A double-solenoid version can remain in its last shifted state until the opposite coil is energized. Neither arrangement is inherently better. The correct choice depends on the required behavior after a control interruption, restart procedure, and whether the actuator must return to a known position.
For 5/3 valves, the center condition deserves special attention. A closed-center valve can hold air on both sides of a cylinder, but this does not guarantee precise mechanical holding because air remains compressible and internal leakage can occur. An exhaust-center configuration can remove force from the actuator, while a pressure-center configuration may keep both sides pressurized. These states affect safety, energy use, recovery after an emergency stop, and the possibility of trapped pressure.
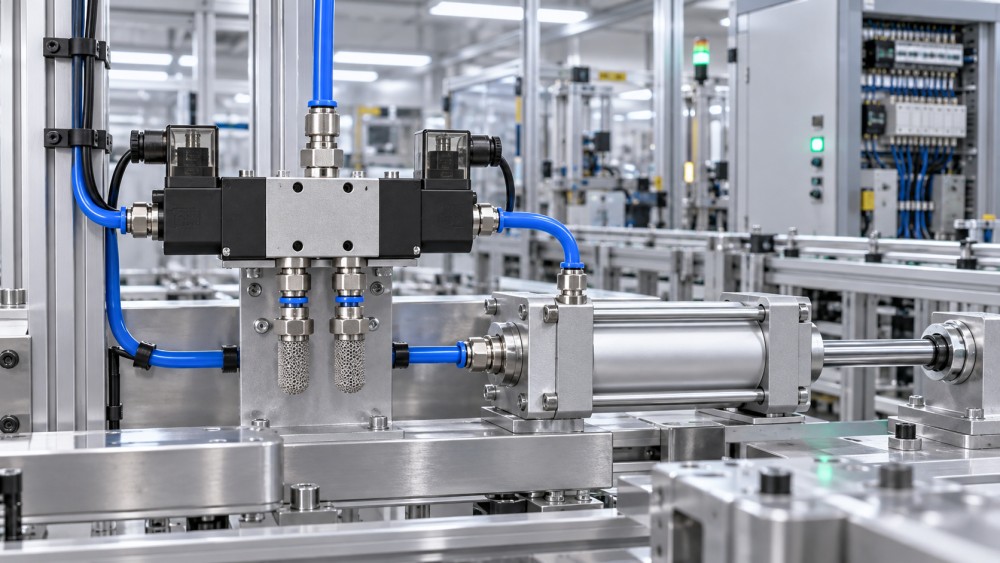
Voltage selection is about the control architecture, not just the coil label
Coil voltage must match the available control power and its real operating condition. Common industrial systems may use AC or DC coils, but an evaluator should not assume that equal nominal voltage means equal electrical behavior. AC and DC solenoids have different operating characteristics, wiring practices, and failure modes.
DC coils are widely used with PLC outputs, remote I/O, mobile electrical systems, and machine control panels because they align well with low-voltage control circuits. Their pull-in behavior depends on the available voltage at the coil terminals. Long cable runs, undersized conductors, corroded connections, weak power supplies, or simultaneous actuation of several loads can reduce terminal voltage enough to prevent reliable shifting. A coil that works during bench testing may become intermittent when installed at the far end of a machine.
AC coils are often used where the control system is built around AC power. Their inrush and holding behavior differs from DC coils, and coil heating must be considered in the expected duty cycle. Replacing an AC coil with a DC coil, or the reverse, simply because the connector fits is not a valid substitution. The valve manufacturer’s approved coil and electrical specification should govern the choice.
Voltage tolerance matters most where the machine has unstable supply conditions, long harnesses, battery power, or many valves energized together. It is also worth checking whether the coil is designed for continuous energization. A valve that remains powered for long periods must dissipate heat in its actual mounting location, not only in open air. Tight manifolds, hot enclosures, direct sun exposure, nearby heaters, and elevated ambient temperature can raise coil temperature significantly.
Electrical protection should be selected as part of the valve assembly. DC coils can generate a voltage transient when de-energized. Suppression devices protect control electronics, but some methods also slow electrical release and can increase valve drop-out time. That trade-off is often overlooked in fast sequences. If a cylinder must release rapidly, confirm the behavior of the coil, connector, and suppression method together instead of adding a generic suppression component after commissioning.
Porting must be read as an airflow path
Port configuration is more than the thread size on the valve body. The air must enter through the supply port, move to the correct work port, and leave through an exhaust route that does not create back pressure or introduce contamination. Incorrect port mapping can cause reversed cylinder movement, failure to shift, poor speed control, or a machine state that does not match its control logic.
Most directional valves use a supply port, one or more actuator ports, and one or more exhaust ports. Depending on the manufacturer, those ports may be identified by numbers, letters, or both. The pneumatic symbol and port diagram are more reliable than relying on a familiar numbering convention from another brand.
Exhaust design is especially important for fast-moving cylinders. A small silencer, restrictive exhaust manifold, long shared exhaust line, or clogged muffler can slow the actuator even when the valve appears adequately sized on the supply side. In some applications, quick-exhaust valves placed close to the cylinder improve speed by exhausting cylinder air locally rather than forcing it back through the directional valve. This is a system decision, not a replacement for selecting adequate valve flow.
Thread style must also be confirmed. Similar-looking ports may use different thread forms, and forcing an incompatible fitting can damage the valve body or create a persistent leak. The port thread, sealing method, tubing outside diameter, fitting bore, and allowable installation torque should all be compatible. A physically larger connection does not automatically improve performance if upstream tubing, fittings, or manifold passages remain restrictive.
Manifold-mounted versus inline valves
Manifold mounting reduces tubing, simplifies wiring, and supports organized valve banks in automated equipment. It is effective when several actuators are concentrated in one area and individual stations need consistent service access. The trade-off is shared supply and exhaust capacity. Several cylinders actuating together can create a pressure drop through the manifold supply path or exhaust back pressure through a shared silencer.
Inline or locally mounted valves can shorten the pneumatic path to a cylinder. They are often useful where rapid actuator response matters, where the machine layout is spread out, or where individual exhaust routing is needed. The installation may require more fittings and wiring, so maintainability should be weighed against response improvement.
Response time is only one part of actuator response
Published response time generally describes how quickly the valve changes state after the electrical signal is applied or removed under stated test conditions. It is useful for comparing candidate valves, but it is not the same as cylinder extension, retraction, clamp engagement, or complete machine cycle time.
The actuator begins moving only after pressure changes sufficiently on the relevant side of the piston. Air must fill or exhaust a volume through the valve and connected plumbing. A large-bore cylinder, long tube run, small fitting, low supply pressure, high external load, or restricted silencer can dominate the delay even when the valve itself shifts quickly.
Response should therefore be considered as a chain:
- Control output changes state.
- The coil develops enough force to move the valve mechanism.
- The valve opens the required supply or exhaust path.
- Air pressure changes in the tubing and cylinder chamber.
- The cylinder overcomes friction, load, and any opposing pressure.
- The moving equipment reaches its intended position or sensor point.
For a high-speed indexing or pick-and-place sequence, evaluate the full chain at the expected operating pressure and cycle rate. A fast valve cannot compensate for undersized tubing or a cylinder selected without considering load and acceleration. Conversely, specifying the fastest available valve for a slow guard actuator may add cost and electrical demand without a practical benefit.
There is also a difference between energization response and de-energization response. In a spring-return valve, the return spring, internal pressure, spool friction, and electrical release behavior all influence the return event. In a double-solenoid valve, the opposite coil must be commanded to change position. The sequence controller needs to reflect that difference, particularly when a safe restart depends on knowing the valve’s actual state.
Flow capacity should be matched to the pneumatic demand
Valve flow ratings are often presented as a flow coefficient, a standardized flow value, or a nominal passage size. These values help comparison, but they must be interpreted using the manufacturer’s stated conditions. Do not compare values from different measurement methods as though they are automatically identical.
A practical selection begins with cylinder air demand and required stroke time. Larger cylinders move more air. Higher cycle rates increase total consumption. The supply network must also support simultaneous demand from other actuators, blow-off functions, vacuum generators, and tools. If supply pressure falls when several devices operate, a correctly selected directional valve may still produce inconsistent motion.
Oversizing deserves some restraint. A much larger valve may provide more flow, but it can make a lightly loaded actuator move too aggressively, increasing impact at end of stroke. Flow controls, cushioning, mechanical stops, and load conditions then become more important. Select capacity for the needed motion and acceptable pressure loss, then tune speed at the actuator where appropriate.
Pressure range, pilot operation, and air quality change the answer
Some pneumatic solenoid valves are direct-acting; the solenoid moves the sealing element directly. Others are pilot-operated, using system air pressure to assist the main switching action. Pilot-operated designs can provide higher flow in a compact package, but they may require a minimum operating pressure or a suitable external pilot arrangement. A valve that depends on pilot pressure may not function correctly during low-pressure startup, pressure decay, or certain vacuum-related duties.
Check both the allowable pressure range and the pressure available at the valve during the least favorable part of the cycle. Supply pressure at the compressor is not necessarily the same as pressure at a remote manifold during simultaneous actuation. Also distinguish between the pressure rating of the directional valve and the working limits of the tubing, fittings, cylinder, filter-regulator, and downstream equipment.
Compressed air quality has a direct effect on service life. Water, oil carryover, rust particles, scale, and debris can cause sticking, leakage, slow shifting, or seal damage. Filtration should suit the valve design and the surrounding pneumatic components. Drains must work, piping should be cleaned after installation work, and lubricated versus non-lubricated operation should follow the valve’s stated requirements. Introducing lubricated air into a system designed for dry service can create a maintenance dependency if lubrication is later removed.
A disciplined evaluation sequence
For a new machine, retrofit, or replacement project, it is efficient to lock down the mechanical and pneumatic requirements before selecting a catalog variant. The following order prevents many avoidable mismatches:
- Define the actuator function, normal position, and required behavior during power loss or air loss.
- Read the circuit symbol and identify the necessary ports, positions, pilot arrangement, and exhaust paths.
- Establish the available control voltage, wiring distance, duty cycle, connector type, and output protection method.
- Estimate required airflow from cylinder size, stroke speed, operating pressure, and simultaneous demand.
- Review installed tubing, fittings, silencers, manifolds, and exhaust routing for restrictions that can erase the benefit of a higher-flow valve.
- Confirm pressure range, air quality, temperature exposure, ingress protection needs, vibration, and access for service.
- Compare response-time data only after the functional and flow requirements are met.
For replacement work, capture the existing valve’s port diagram, coil marking, mounting interface, connector arrangement, and circuit behavior before removing it. A replacement that appears dimensionally compatible may reverse the normal state, use a different pilot requirement, or place the ports differently. This is particularly relevant for manifold systems where a valve station may look identical to adjacent stations but serve a different actuator function.
IMPE’s coverage of pneumatic actuators, directional valves, air preparation units, and industrial fluid-power systems reflects this wider selection logic: valve choice has to be evaluated as part of the motion, air supply, controls, and maintenance environment. A reliable result comes from matching the complete operating condition rather than selecting from one headline specification.
Questions that should be settled before approval
Does a higher coil voltage make the valve faster?
Not as a general rule. Response depends on the coil and valve design, actual terminal voltage, internal mechanism, pilot conditions, and electrical suppression. Use the specified coil voltage for the control system and evaluate the manufacturer’s response data for that exact configuration.
Can a 3/2 valve operate a double-acting cylinder?
Not by itself in the normal directional-control arrangement. A double-acting cylinder needs controlled pressure and exhaust paths for both sides. A 5/2 or 5/3 directional valve is commonly used because it can alternately pressurize each cylinder chamber.
Why does a cylinder move slowly even though the valve has switched?
The restriction may be downstream or on the exhaust side. Check tubing length and bore, fittings, speed controllers, silencers, shared exhaust lines, cylinder load, supply pressure under demand, and contamination before concluding that the valve is faulty.
Is a bistable double-solenoid valve suitable where a defined fail state is required?
It may not be. Because it can retain its last commanded position, it does not inherently return to a default state after electrical power is removed. Where a known return condition is required, a spring-return design or a separately engineered safety function may be more appropriate.
Related News
- How to Assess a Rigid Coupling Supplier for Bore Accuracy and Traceable QualityOct 08, 2026Tribology & Kinematics Expert
- Titanium Alloys Compared: Balancing Strength, Corrosion Resistance, and MachinabilityOct 08, 2026CNC Kinematics Architect
- Where Ductile Iron Dismantling Joints Reduce Alignment Risk in Water PipelinesOct 08, 2026Pipeline Metallurgy Scientist
- Selecting a Precision Bearing Sleeve: Fits, Runout, and Material ChoicesOct 08, 2026Tribology & Kinematics Expert
- Face Milling Cutters: How Insert Geometry Affects Finish on Steel and AluminumOct 08, 2026CNC Kinematics Architect
- Single-Acting Cylinders for Clamping: Stroke, Force, and Return Spring ConsiderationsOct 07, 2026Fluid Power Control Strategist